Home › Cutting Services
26 automatic bandsaw machines and high-speed circular saws in Klang — cutting steel rods, pipes, plate and profiles up to 1,000 mm diameter, 10 metric tons a day, with no minimum order.
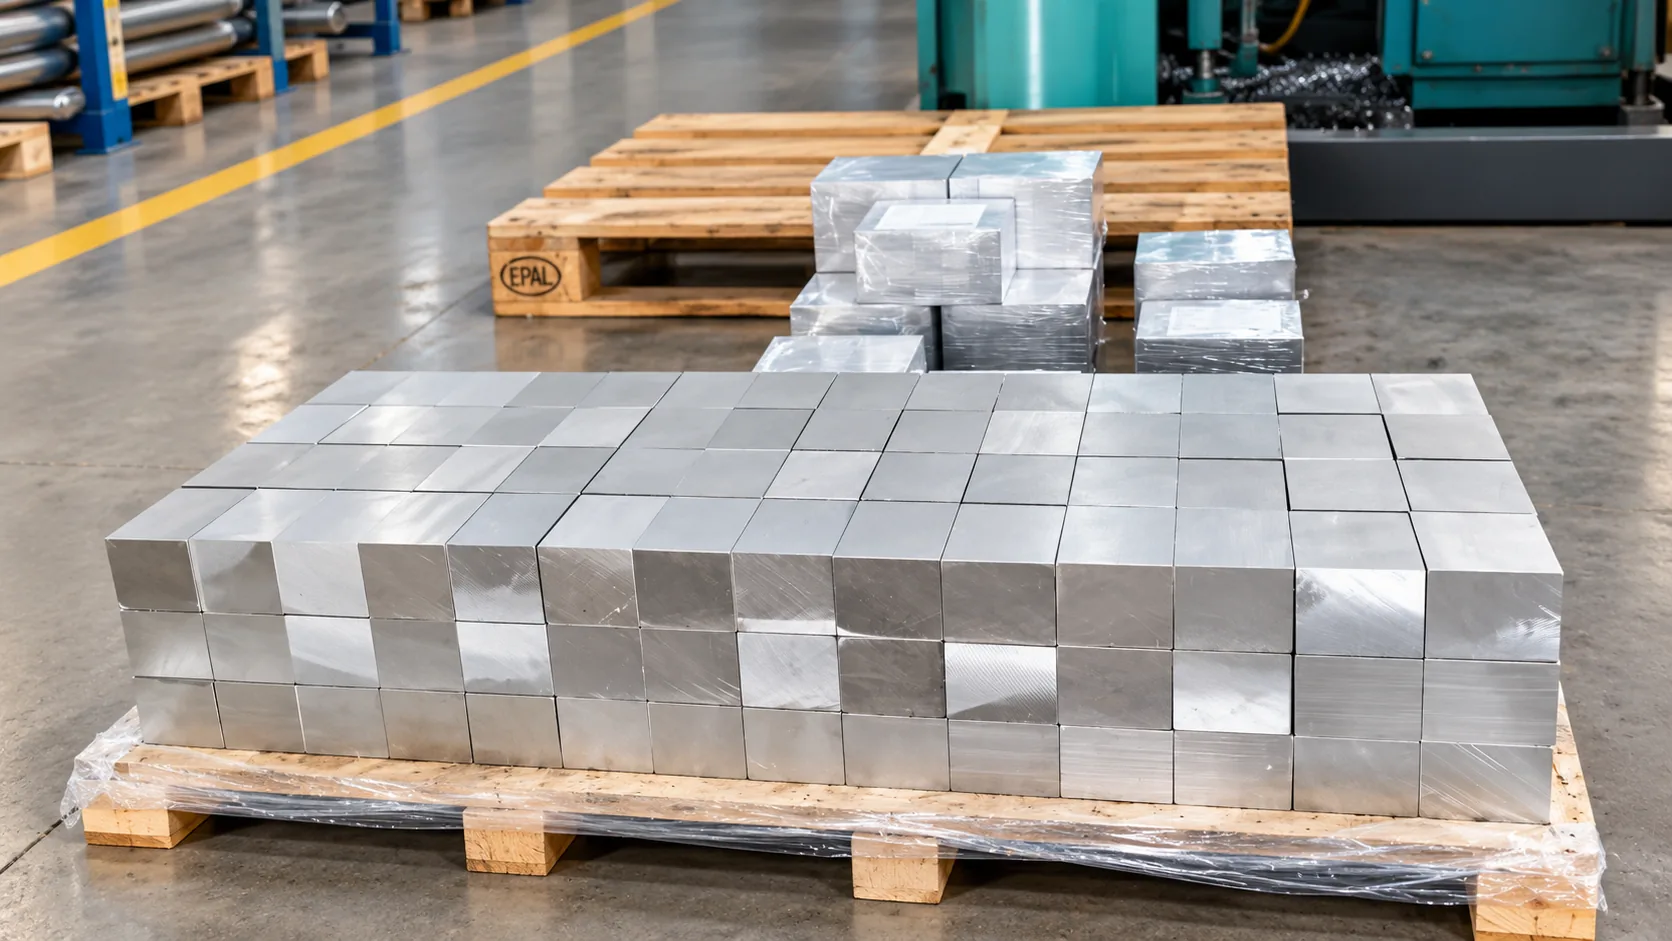
E STEEL SDN BHD runs its own cutting floor alongside the warehouse, so the material you order leaves us at the size your job actually needs. We specialise in bandsaw cutting for a wide range of metals up to 1,000 mm diameter — round bar, hollow bar, pipe, plate, angle, channel and beam.
Bandsawing is a cold-cutting process. A continuous toothed blade shears the material grain by grain, so there is no heat-affected zone, no oxidised edge and no thermal distortion — the metal that reaches your CNC is metallurgically identical to the parent plate.
Order one piece or a thousand — cutting is quoted together with the material.
Clean, burr-free edges that go straight to semi-finishing, skipping the roughing pass.
Against 3–6 mm for plasma and laser — a real saving on expensive alloys.
Send the dimension and quantity; in-stock cutting lists are answered the same business day.
Automatic bandsaw machines
High Speed Circular Saw
Vertical bandsaws
Cut every day
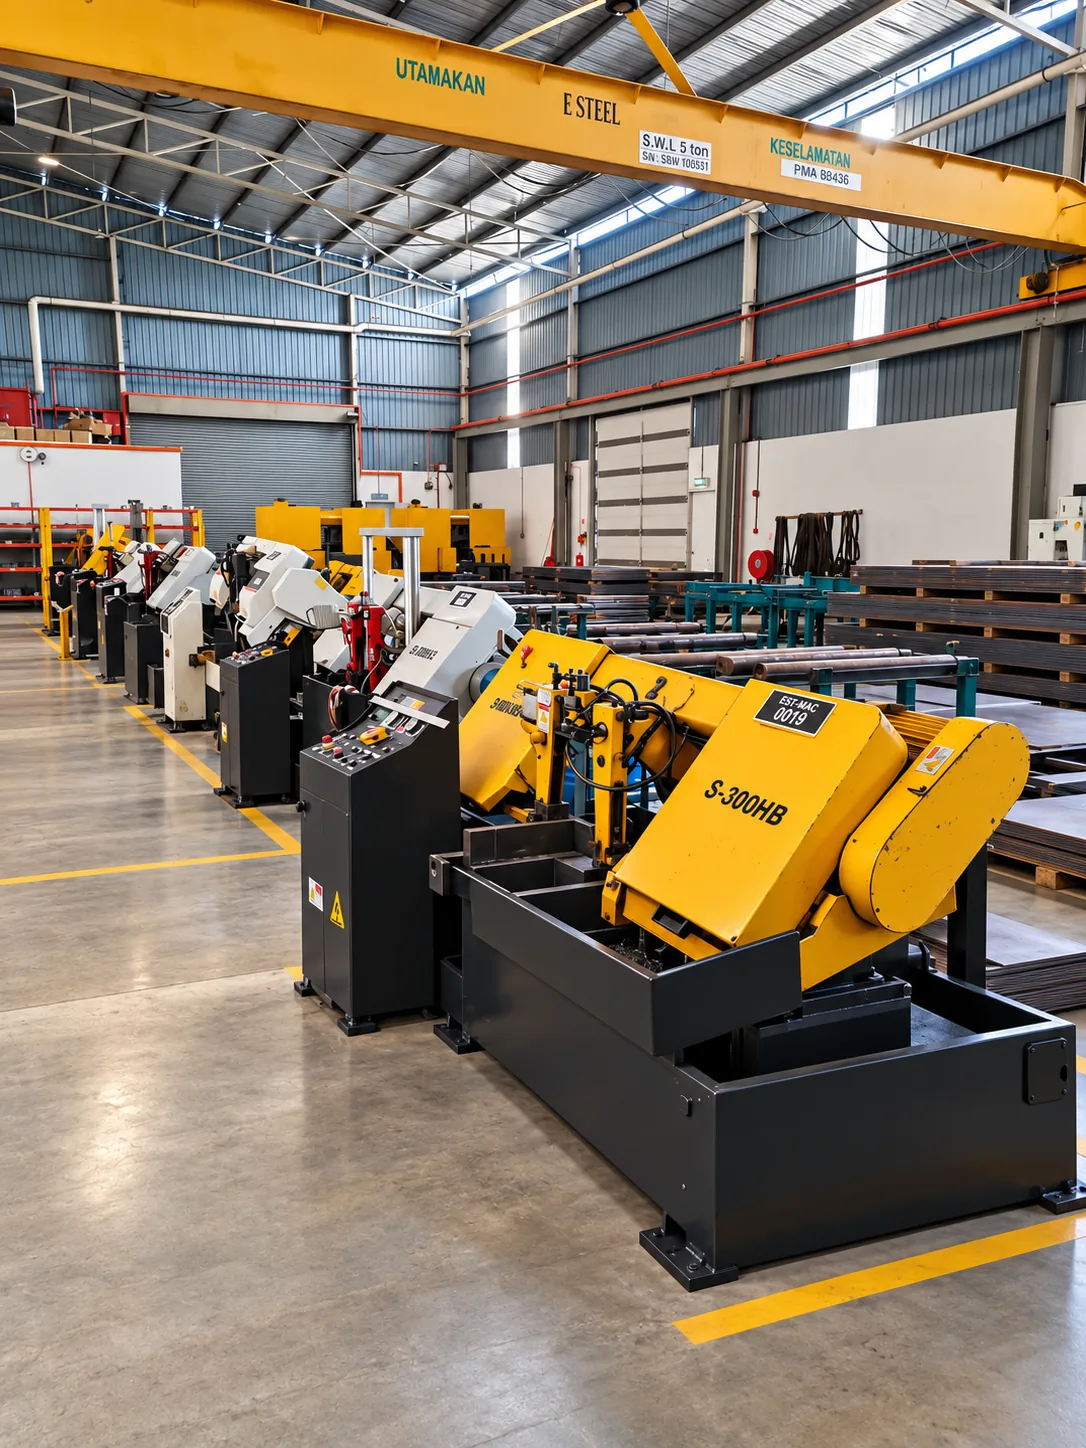
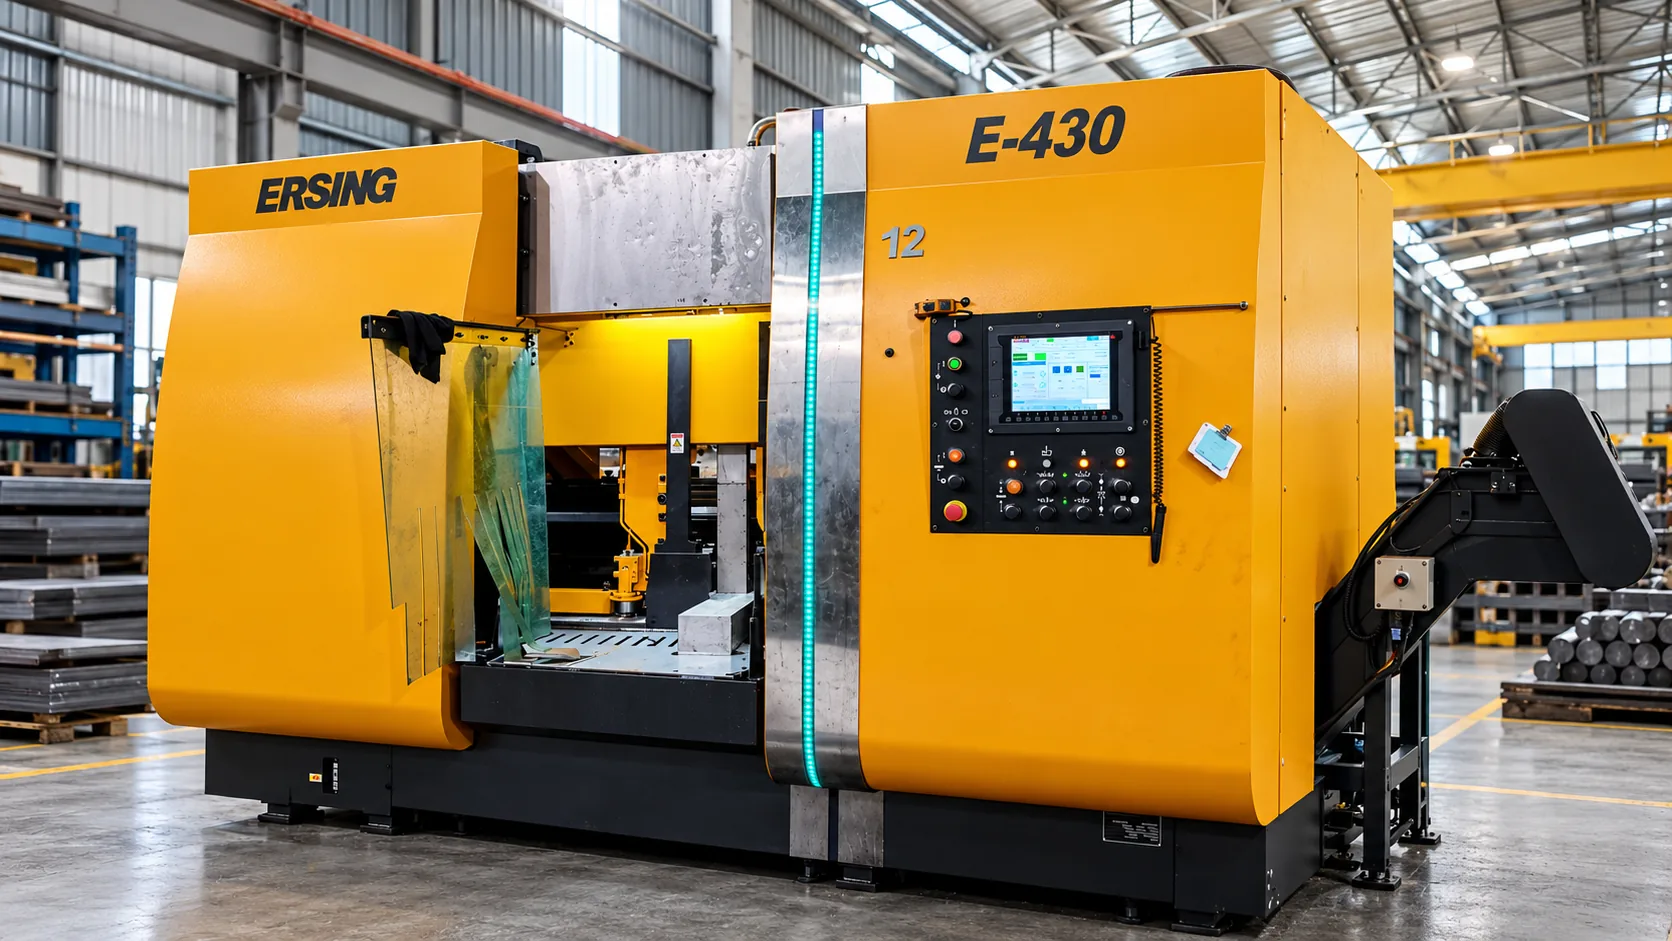
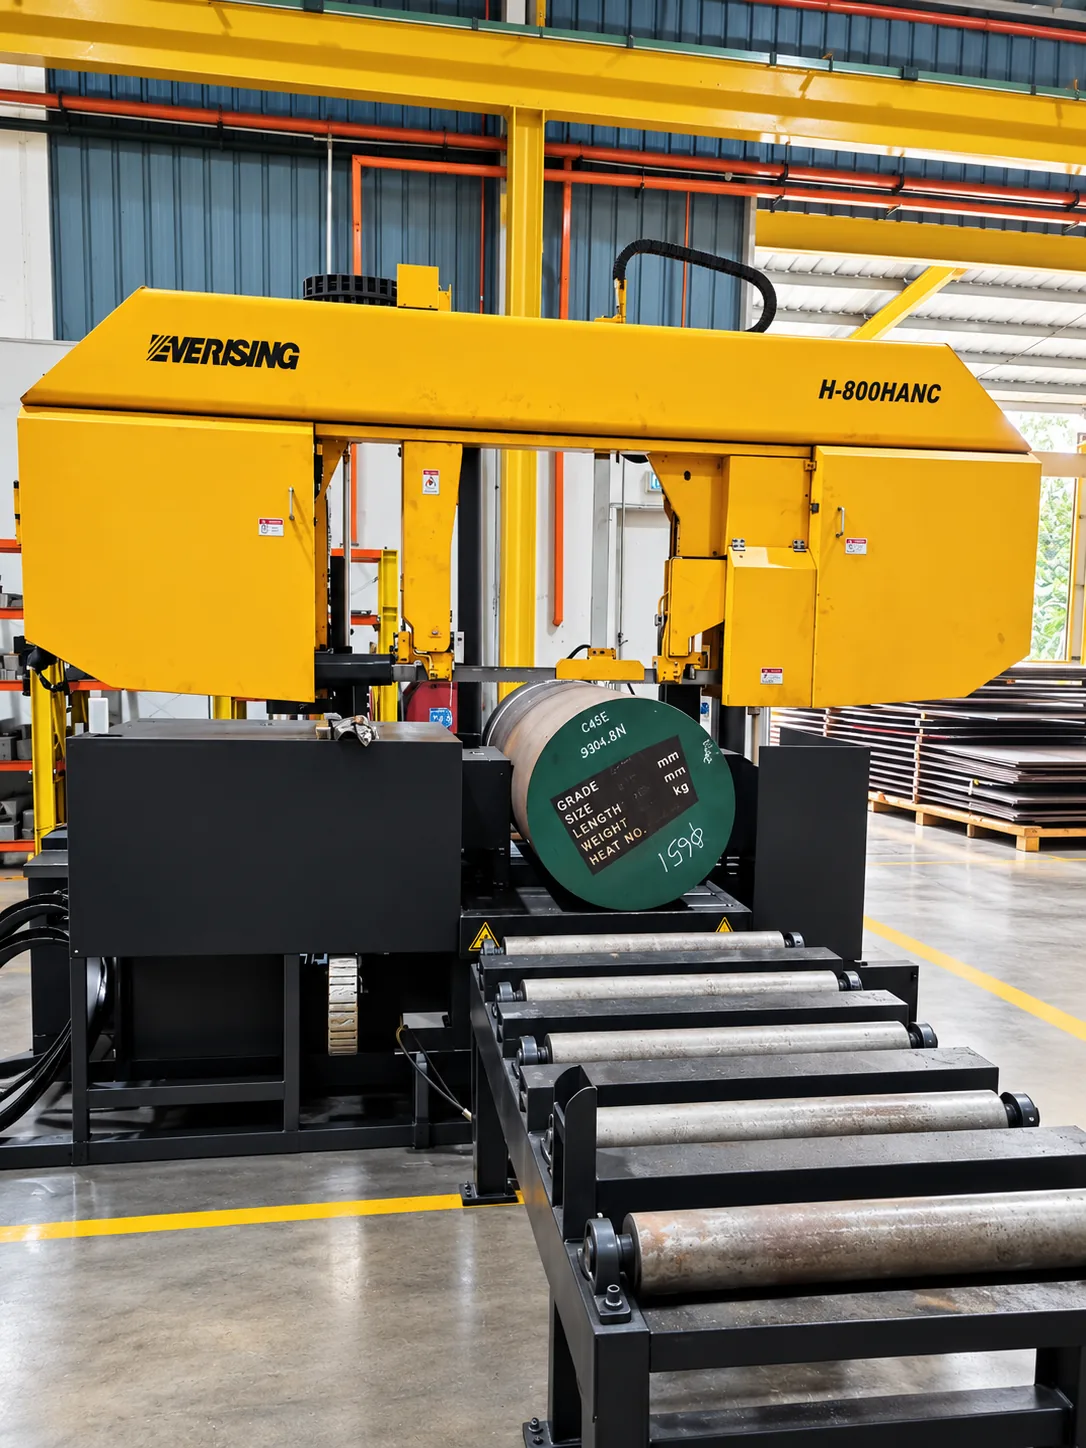
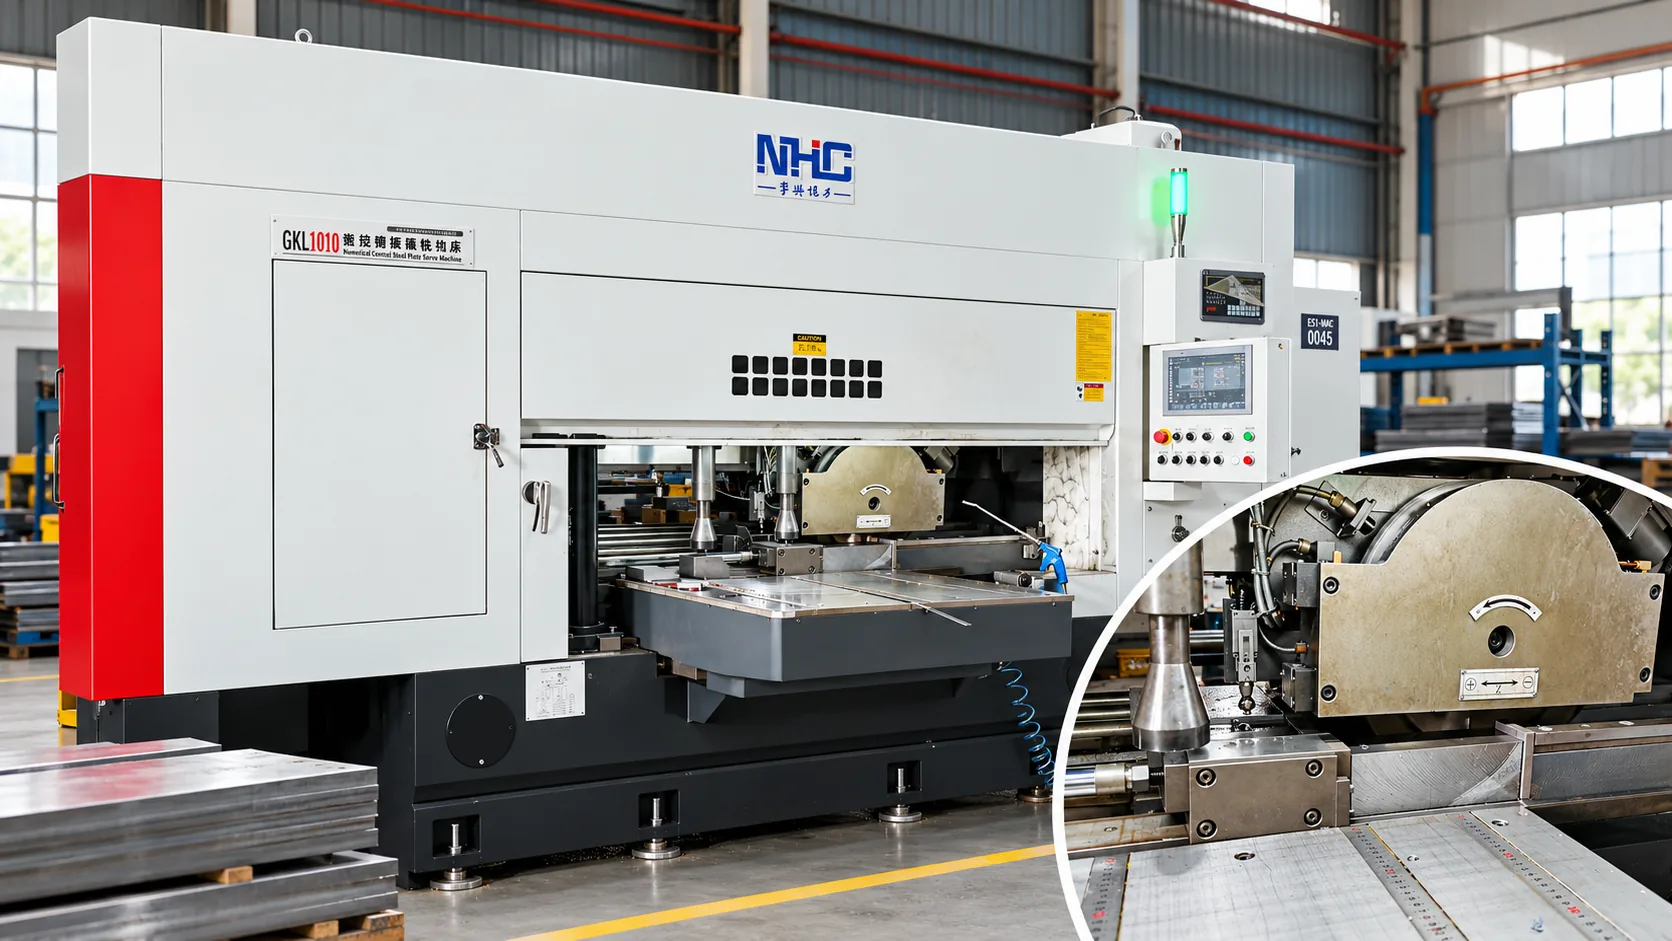
Twenty-three automatic horizontal bandsaws handle the bulk of our work — round bar, hollow bar, API pipe, angle, channel and beam, in diameters up to 1,000 mm (39.4 in). Auto-feed keeps every piece in a batch identical, which is what makes repeat orders and long cutting lists economical.
Because the cut is cold, thick sections come off the saw without the taper, dross or hardened skin that thermal methods leave behind.
| Units in operation | 23 |
| Maximum diameter | Ø1,000 mm (39.4 in) |
| Tolerance | ±1.0 mm |
| Typical work | Round bar · Hollow bar · Pipe · Profile |
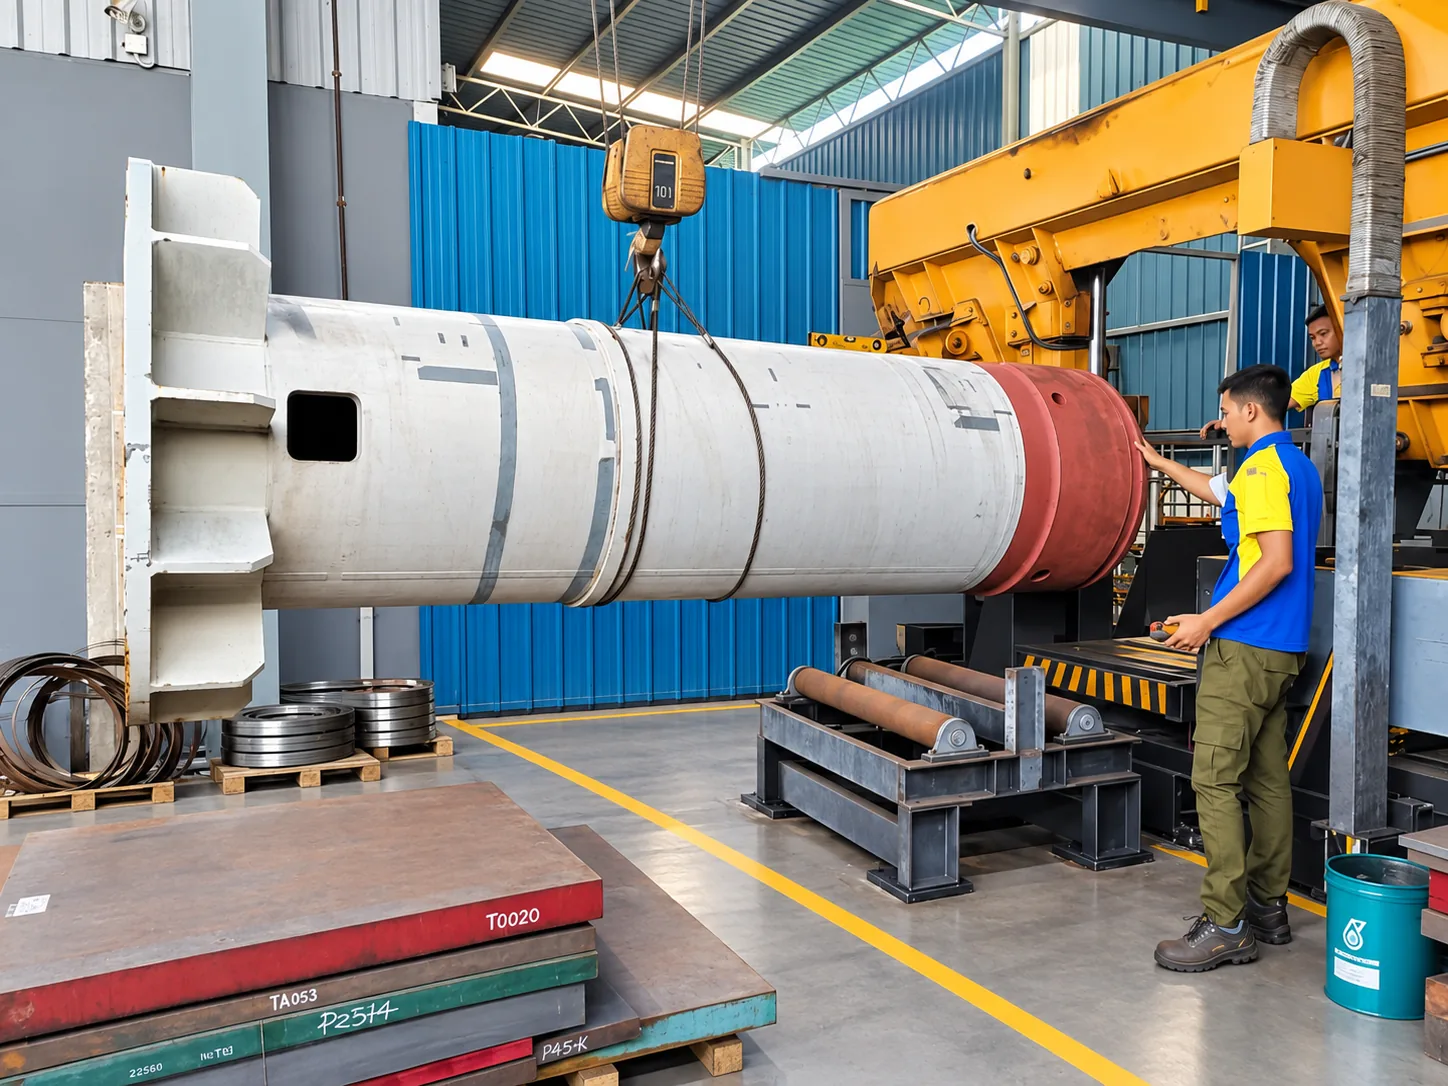
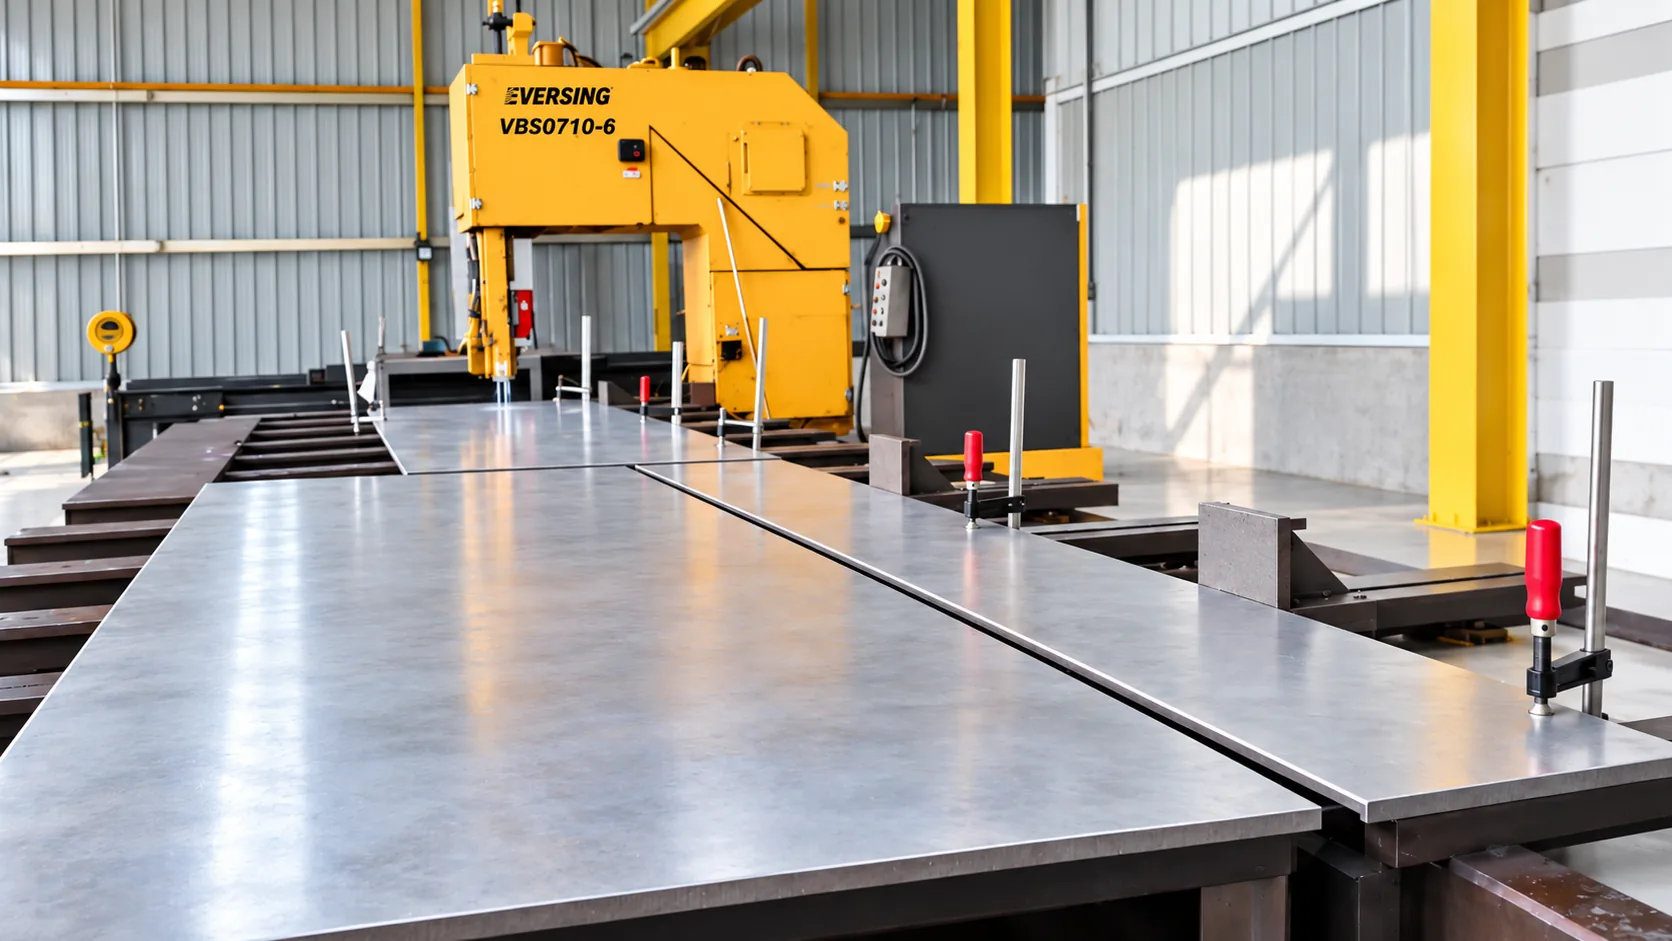
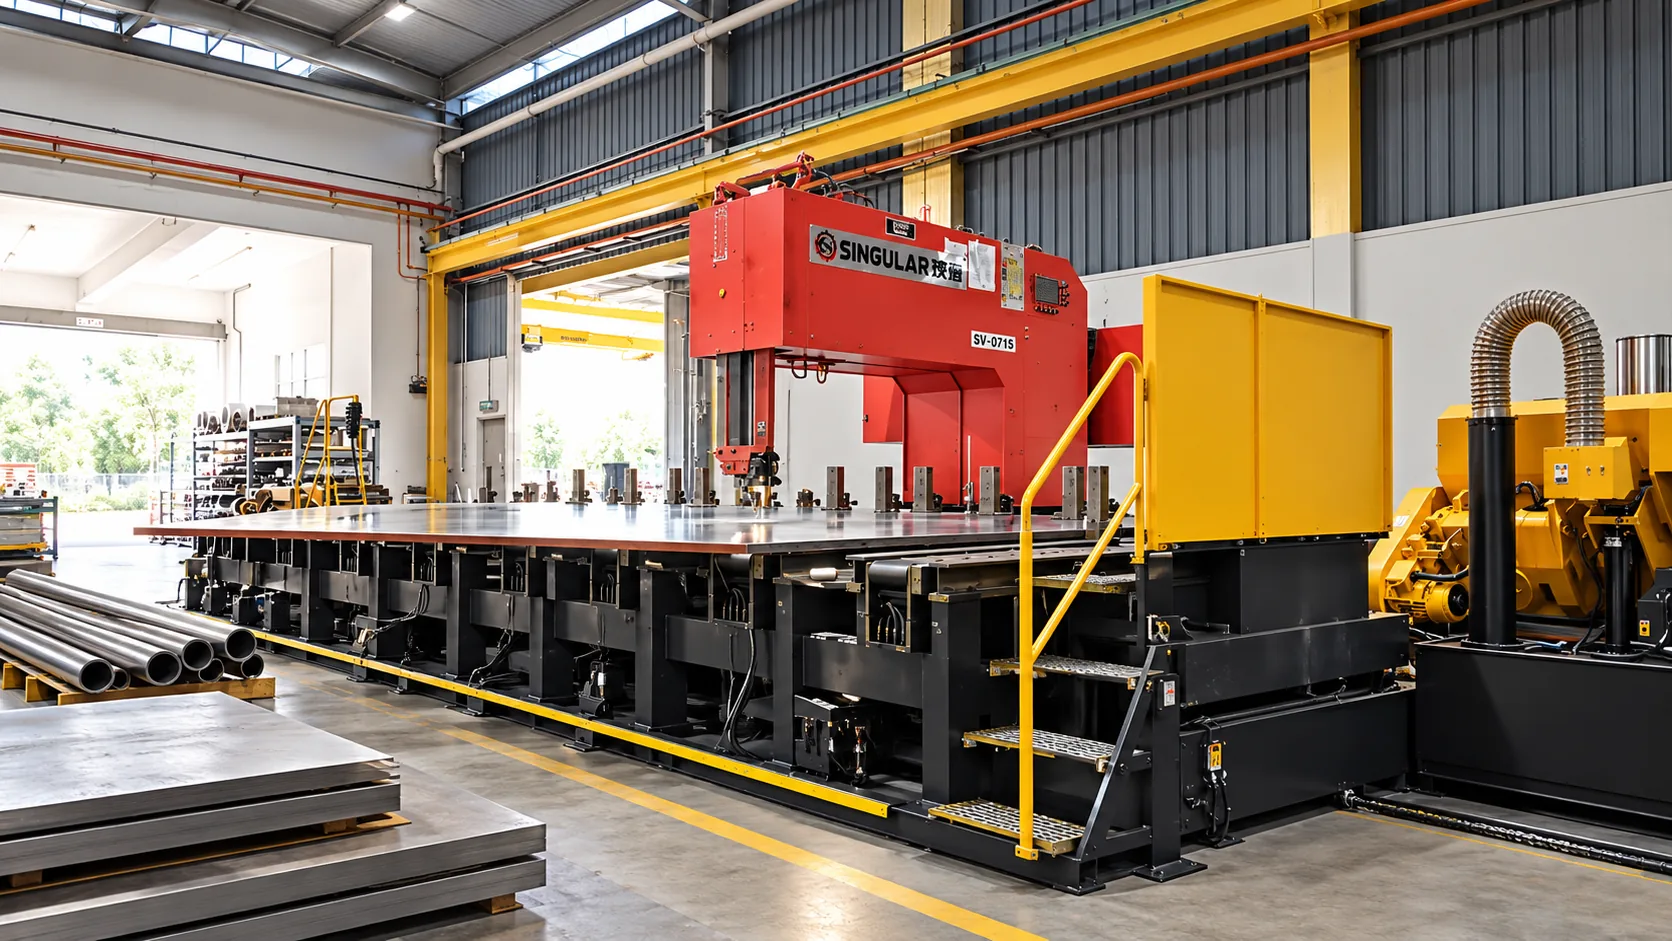
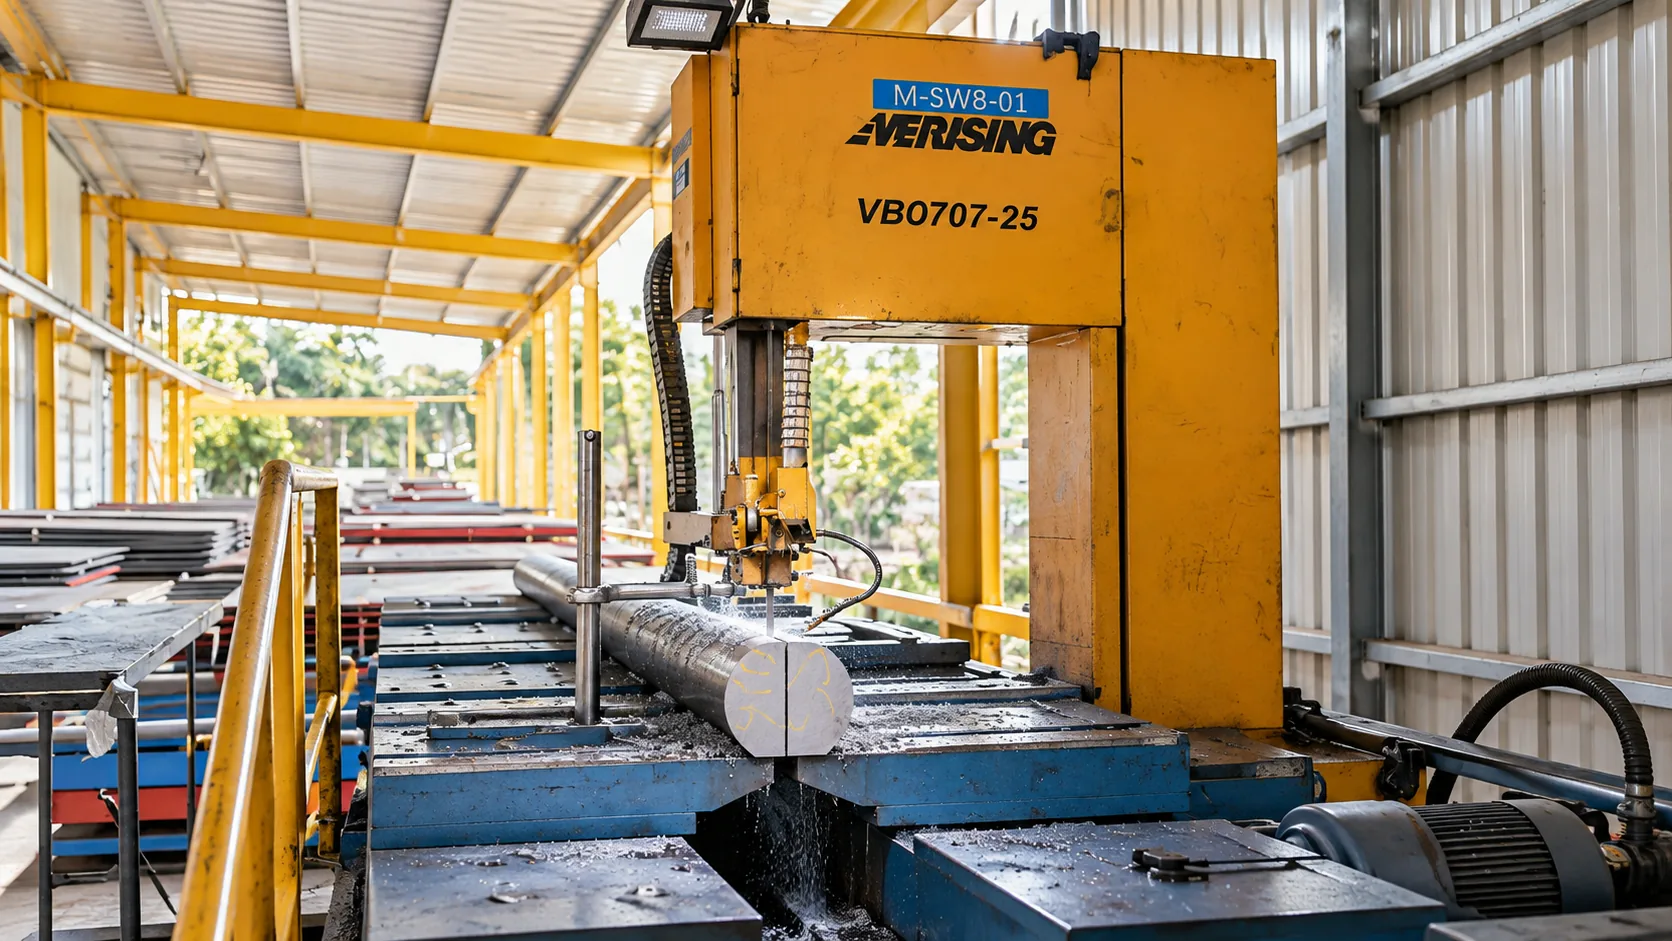
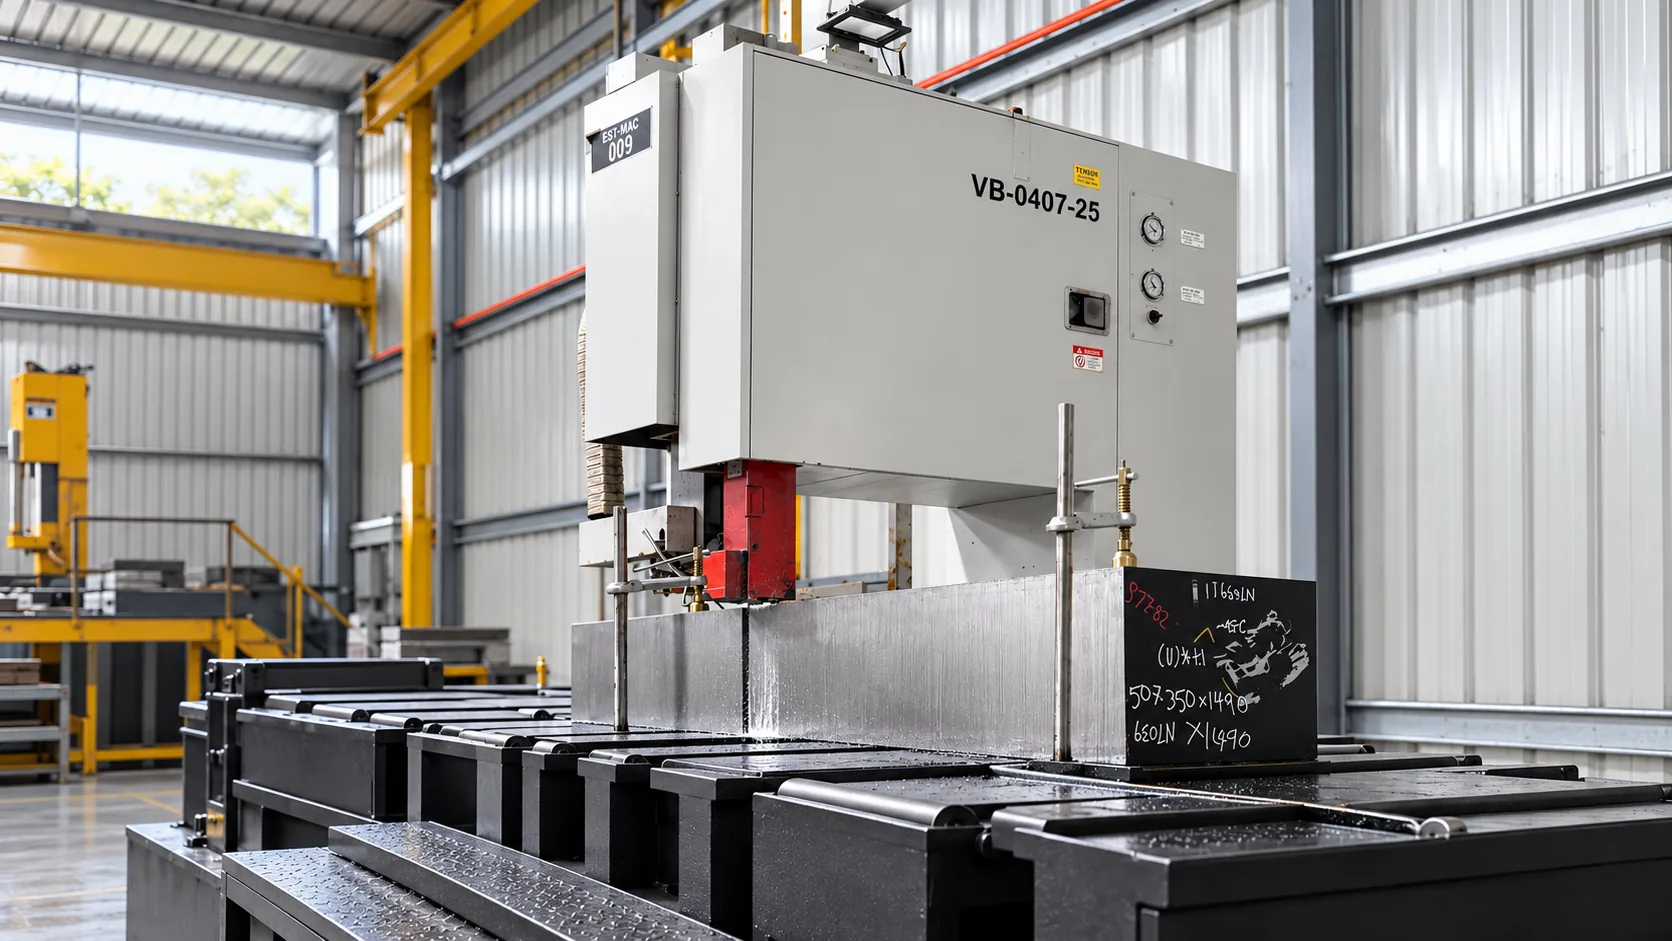
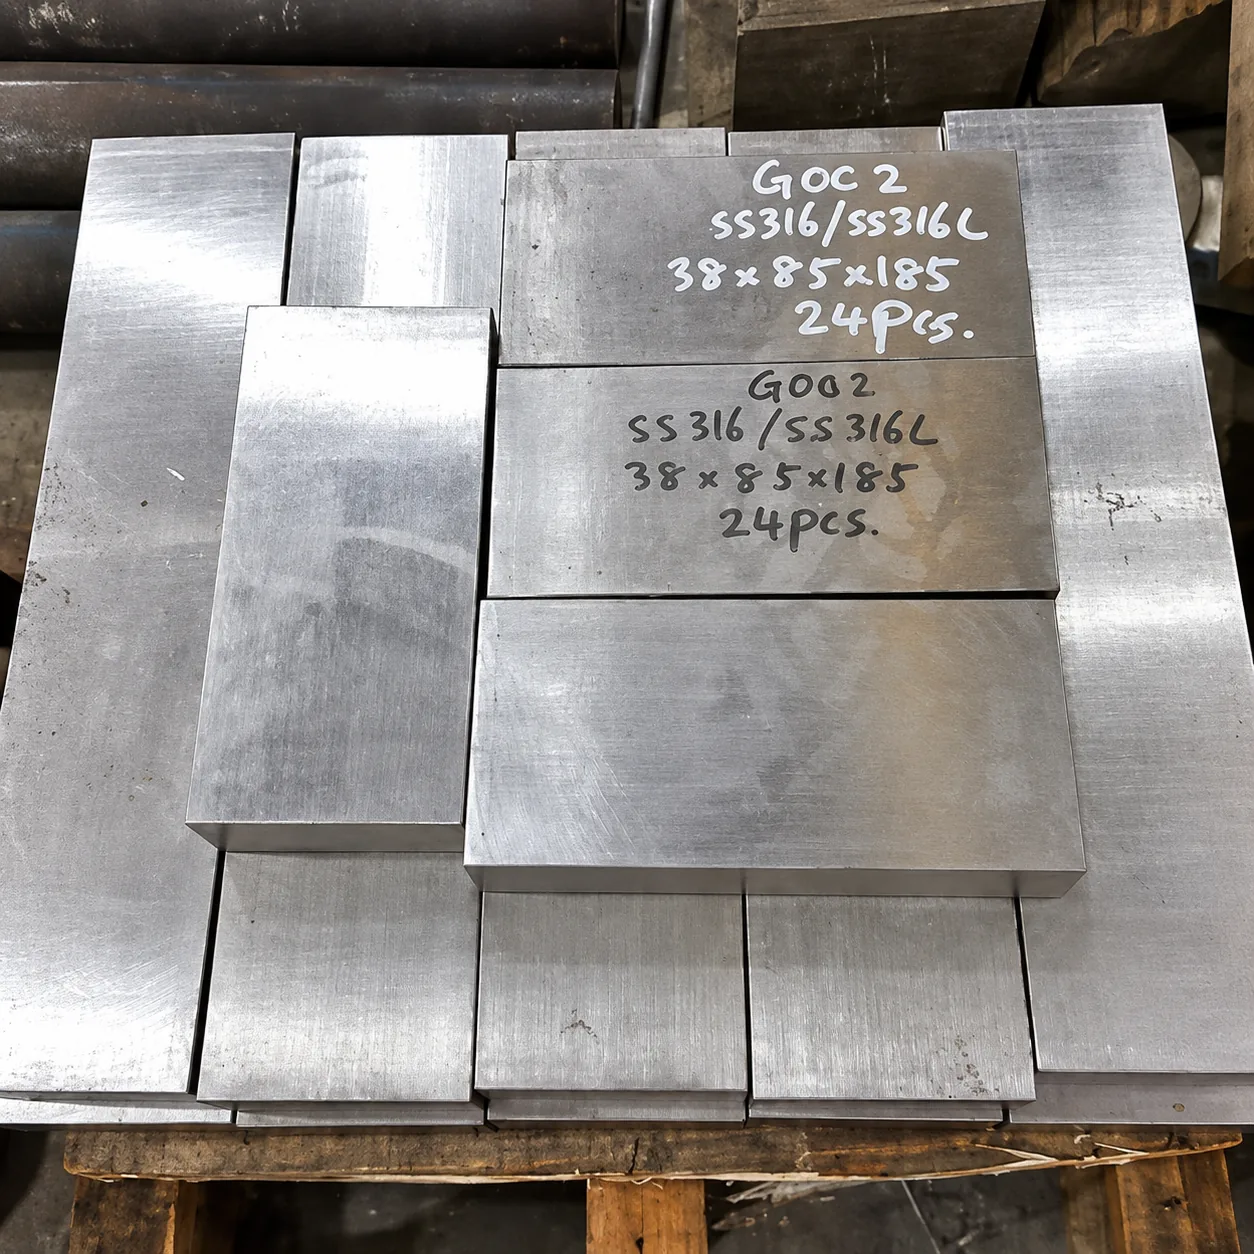
Three vertical bandsaws take plate up to 1,500 × 4,000 mm (59″ × 157″). This is where we cut structural, marine and abrasion-resistant plate into blanks, and where the more unusual jobs happen — converting a round bar into a rectangular block, or a plate into a hexagon.
Clean edges and minimal waste matter most here, because plate in these grades is expensive and a wide kerf is money on the floor.
| Units in operation | 3 |
| Maximum plate size | 1,500 × 4,000 mm |
| Kerf width | 1–2 mm |
| Specialities | Round to plate · Plate to hexagon |
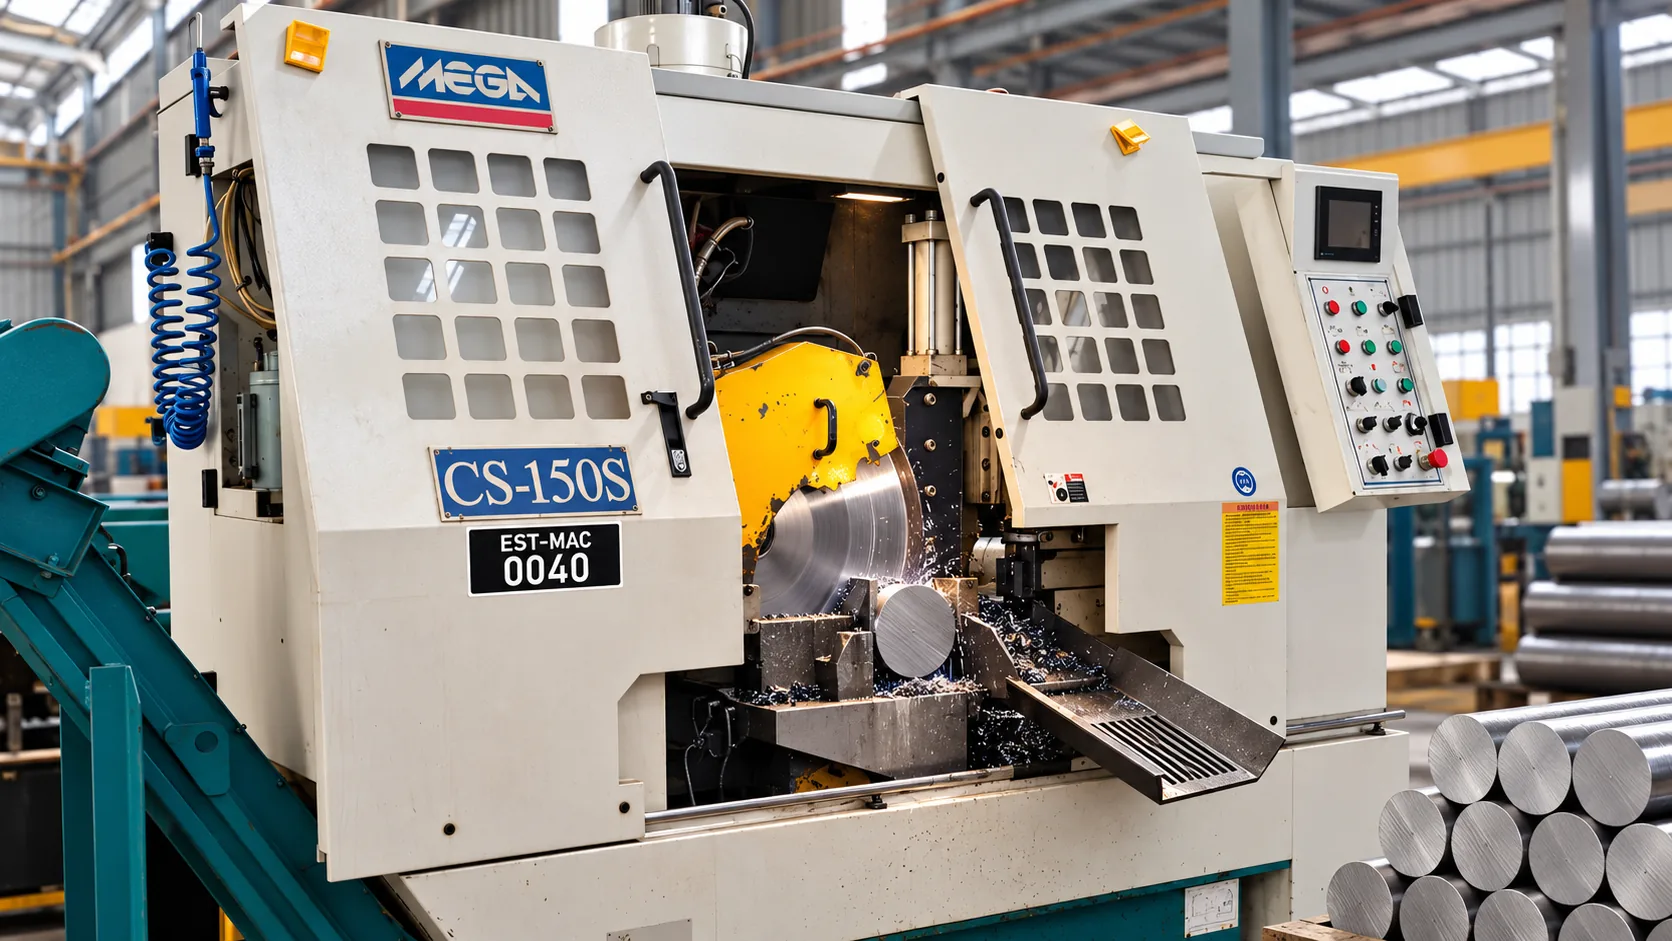
For high-volume repeat work on smaller diameters, a high-speed circular saw finishes a cut in a fraction of the time a bandsaw takes, with a finer surface straight off the blade. We use it where a long cutting list has to ship quickly and the finish has to be good enough to machine immediately.
It is the right tool for bulk order volumes; for thick sections and the widest range of grades, the bandsaws still lead.
| Best for | Bulk volume, smaller diameters |
| Cut speed | High — seconds per cut |
| Surface finish | Fine, ready to machine |
| Process | Cold cut — no heat-affected zone |
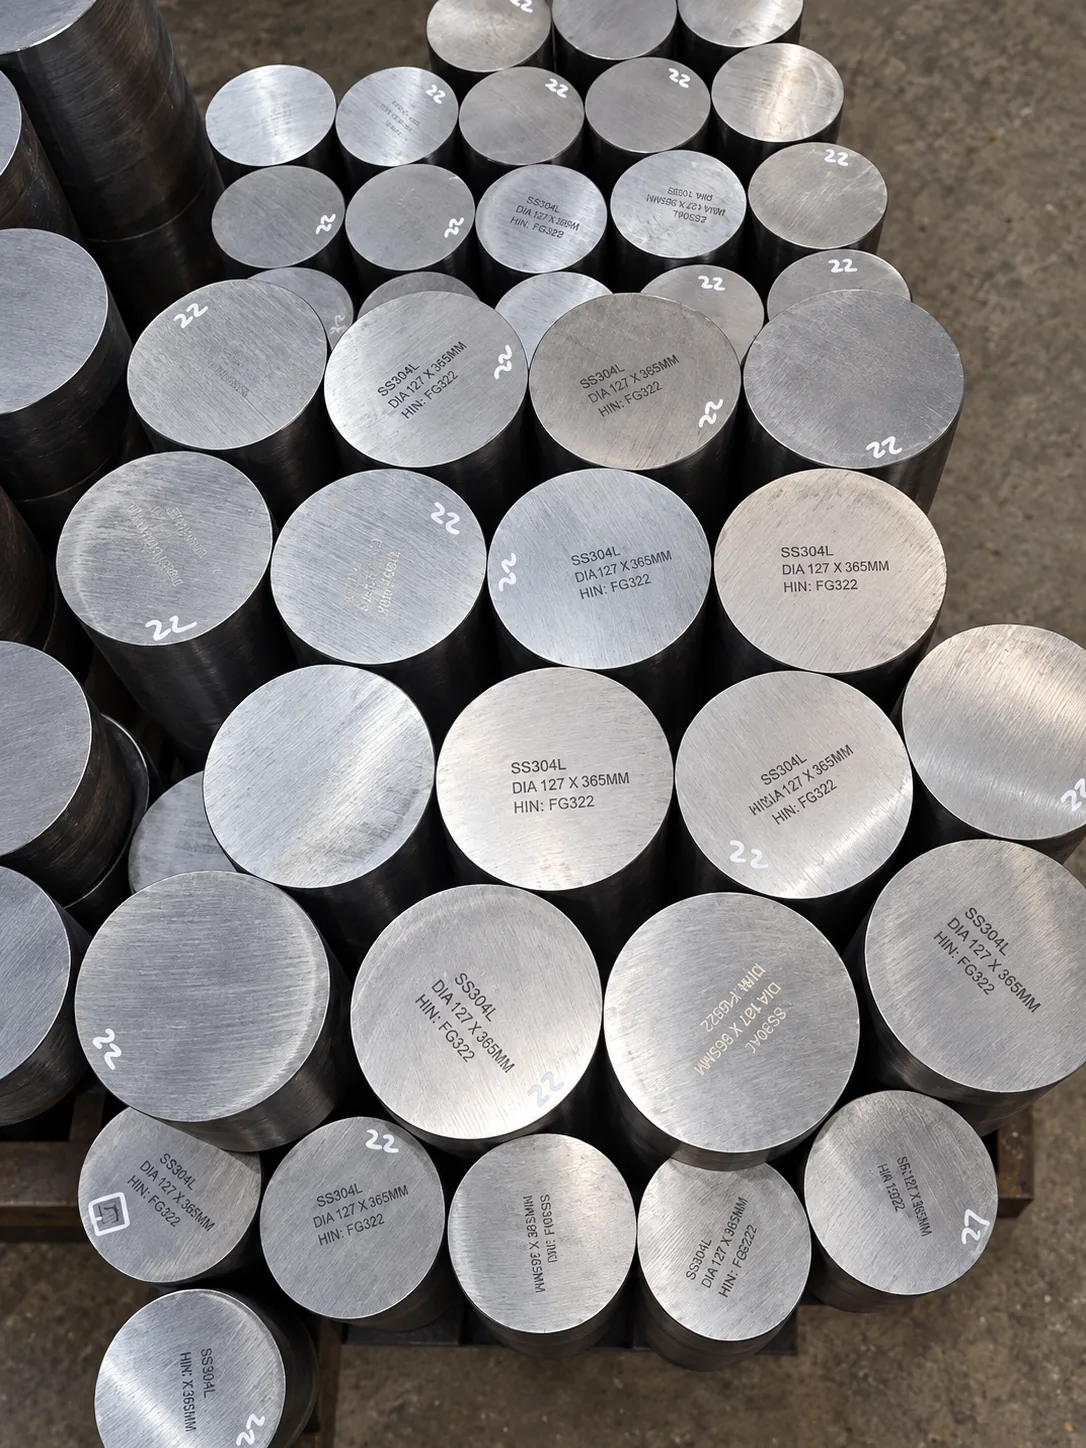
Laser and plasma are excellent on thin sheet. Once the section gets thick, the heat-affected zone and the wide kerf start costing more than the cut saves.
| Factor | Bandsaw (E Steel) | Plasma | Laser |
|---|---|---|---|
| Cutting accuracy | ±1.0 mm | ±1.5–3 mm | Tight on thin sheet |
| Material thickness | Up to Ø1,000 mm | Up to ~100 mm | Limited to ~100 mm |
| Kerf / waste | 1–2 mm | 3–6 mm | 3–6 mm |
| Thermal impact | Cold cut — none | HAZ, oxidised edge | HAZ, risk of warping |
| Edge quality | Smooth, burr-free | Rough, needs deburring | Dross and recast layer |
| Cost on thick sections | Lowest for bulk orders | Higher — gas, consumables | Highest — energy, gas |
| Best suited to | Thick sections, tight specs, volume | Thin sheet, rapid prototyping | Thin sheet, intricate profiles |
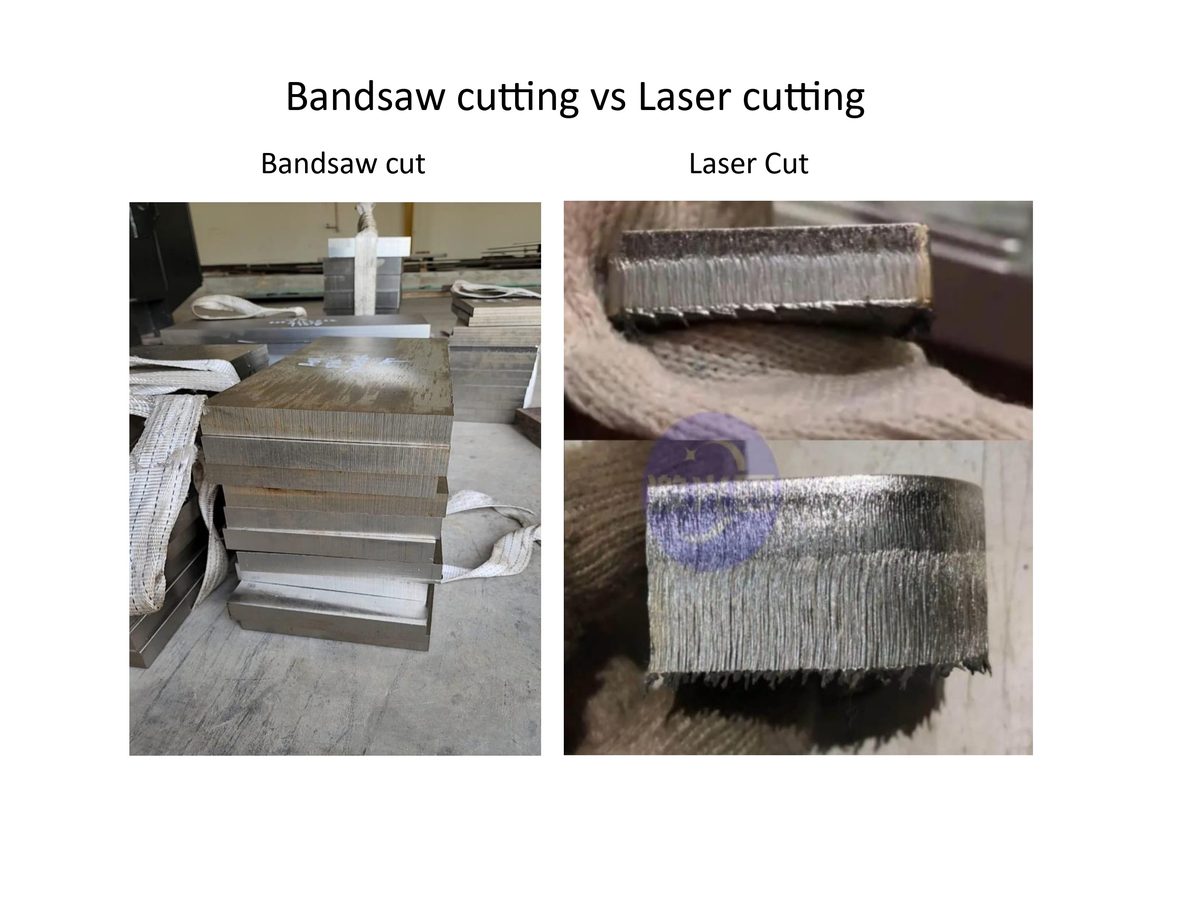
A laser cutting thick stainless leaves a hardened, oxidised layer at the edge. Your toolpath has to remove 1–3 mm of abrasive material before any finishing can start — a roughing pass that adds nothing to the part.
A bandsaw-cut blank at +1 / −0 mm arrives clean and unhardened, so machining can begin at semi-finishing. That is why semiconductor and vacuum-component makers specify bandsaw-cut stock.
Bandsaw cutting to your required sizes across the full range of materials we hold — and a few we do not, if you supply the stock.
Send the dimension and the quantity. We confirm the material, the cutting and the price — then cut, document and ship.
Grade, dimensions and quantity — or attach the drawing. No minimum order applies.
Competitive pricing within 24 hours, with the cutting quoted together with the material.
Cut to ±1.0 mm, checked, and issued with a Mill Test Certificate for the material.
Across Malaysia and ASEAN, by sea or air freight where the lead time matters more.
Thick-walled pipe, flanges, valve bodies and downhole components where material traceability is mandatory.
Vacuum chambers, gas distribution manifolds and process tool parts that need stock free of any heat-affected zone.
Hull sections, marine fittings and classification-grade plate cut to the yard’s nesting list.
Structural beams, base plates and brackets cut from A36, S275 and S355 stock.
Axles, shafts and chassis components blanked from alloy and case-hardening steel.
Custom-cut profiles for machinery, tooling, jigs and maintenance work of every size.
No. We cut material we supply and material you send in. If we supply it, the cutting is quoted together with the material and there is no minimum order on either.
±1.0 mm as standard across the bandsaw fleet. For blanks going straight to CNC we commonly work to +1 / −0 mm so the part is always oversize, never undersize, and the roughing pass can be dropped.
Up to 1,000 mm diameter on the horizontal bandsaws, and plate up to 1,500 × 4,000 mm on the verticals. That is roughly ten times what plasma or laser will handle on stainless.
Thermal cutting hardens and oxidises the cut edge. That layer is abrasive, so your toolpath has to remove 1–3 mm before finishing can start — wasting cycle time and tooling. A cold-cut edge has no such layer, which is why semiconductor and vacuum work specifies it.
Quotations go out within 24 hours, and enquiries on in-stock items received before 6:00 PM are answered the same business day. Our floor processes about 10 metric tons daily, so volume rarely changes the schedule.
Yes — aluminium, copper, nickel alloys, titanium and engineering plastics such as Teflon and Delrin all run on the same machines.
Dimensions and quantity are enough to start. Cutting is quoted with the material, and in-stock enquiries before 6:00 PM are answered the same business day.